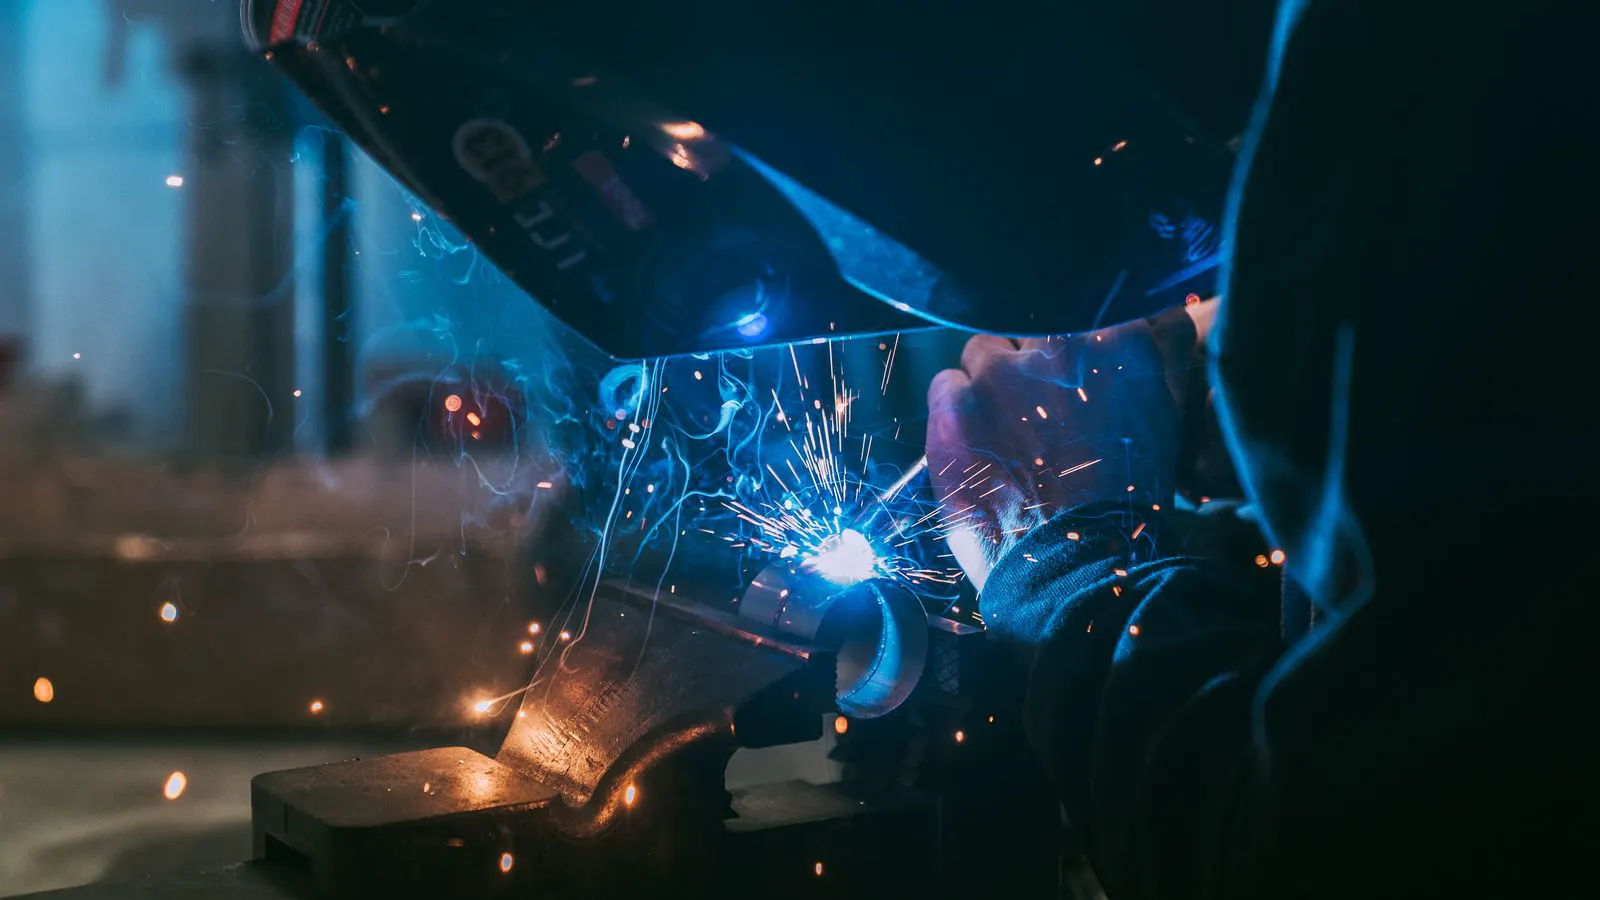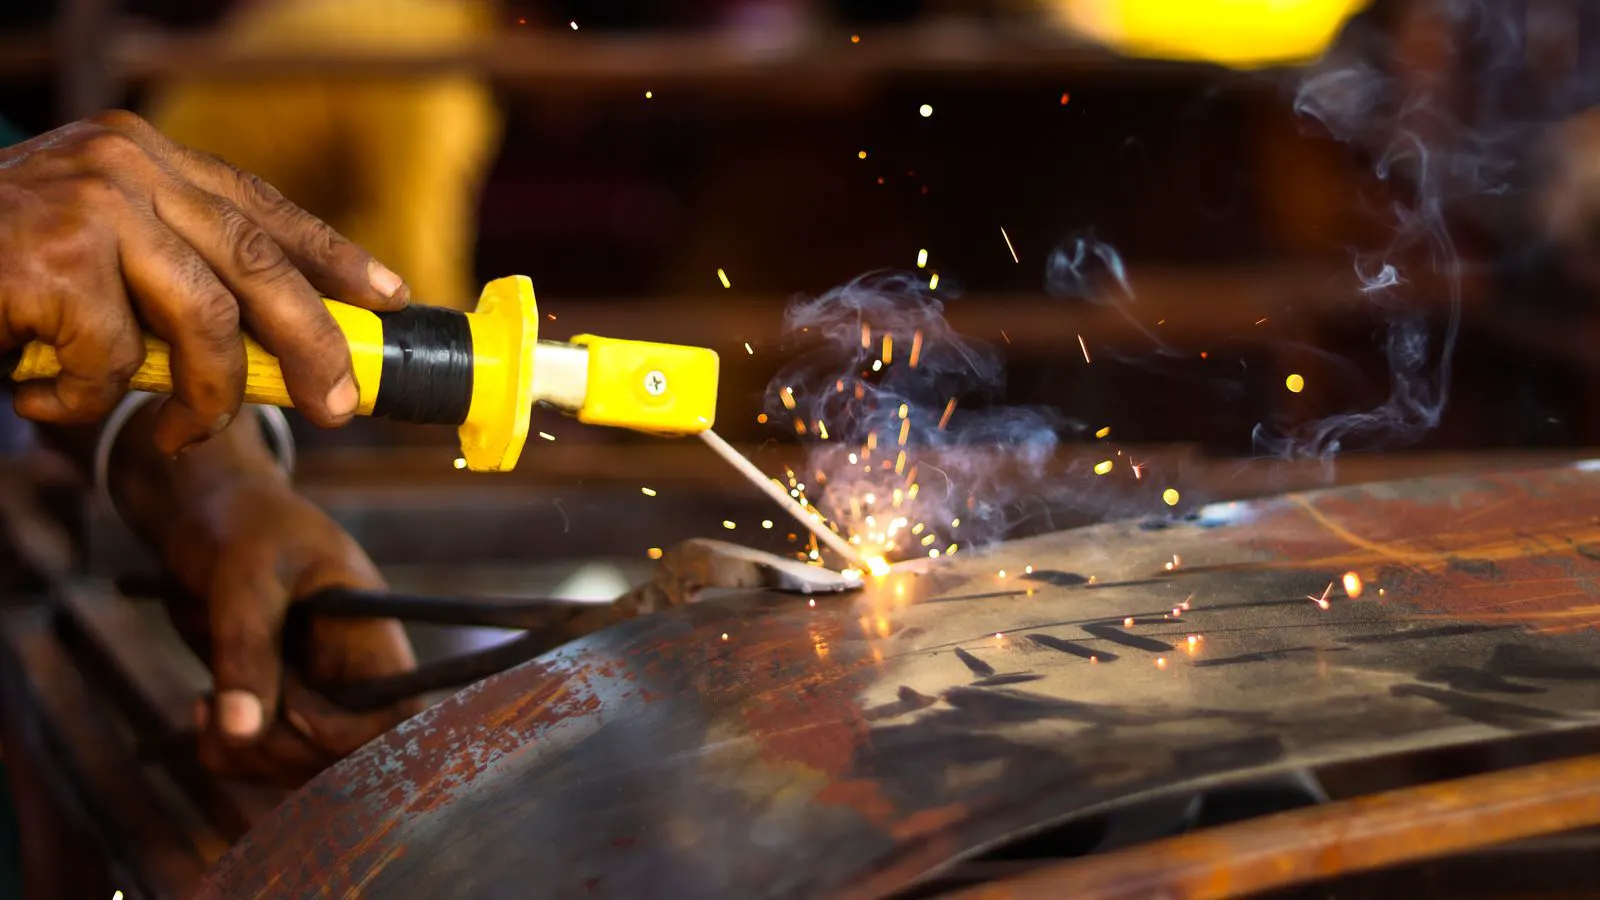
Engineers select electrodes by matching the coating chemistry to the steel grade, joint design, and position. This guide breaks down the criteria for choosing structural steel electrodes for load-bearing work.
- Match electrode classification to the base metal grade and hydrogen content limits.
- Coating chemistry determines arc stability, spatter, and the ability to weld in vertical or overhead positions.
- Always verify mill test reports for consumables to prevent porosity in critical joints.
Selecting the right stick electrode is a decision that directly affects the strength of the finished joint. In structural steel fabrication, a single bad choice can introduce hydrogen, cause cracking, or create a weld that fails inspection. The decision process is not about finding the most expensive rod. It is about matching the electrode chemistry to the steel you are welding, the joint geometry, and the welding position.
Understanding Electrode Classifications
The first step in any electrode choices decision is reading the classification. For low-alloy steel, the 7018 and 6013 designations are common. The first number indicates the tensile strength of the weld metal in thousands of pounds per square inch. The last two numbers describe the coating and the welding position it supports.
The 7018 is a low-hydrogen, high-iron powder electrode. It is used for thick sections and high-strength steel. The coating is designed to remove hydrogen from the arc. This makes it suitable for critical load-bearing structures. The 6013 is a cellulose electrode. It produces a very stable arc and is easy to strike. However, it is not low-hydrogen. It is typically used for thinner sections or where accessibility is difficult.
The 7016 is another low-hydrogen option. It is similar to the 7018 but often has a slightly different coating recipe. It may be easier to strike in certain conditions. The choice between 7016 and 7018 often comes down to availability and specific shop requirements. For high-strength steel, 7018 remains the standard.
Coating Chemistry and Arc Behavior
The coating is not just packaging. It is an active ingredient in the welding process. The flux in the coating breaks down during the arc. It provides the shielding gas and adds alloying elements to the molten pool. It also controls the spatter and the wetting of the base metal.
Cellulose electrodes, like 6013, have a high cellulose content. This creates a lot of gas. The arc is stiff and stable. The spatter is low. This makes it easy to weld in all positions. The downside is the hydrogen content. The cellulose burns down and releases hydrogen. This can cause delayed cracking, known as hydrogen embrittlement.
Low-hydrogen electrodes, like 7018, have a different composition. They use iron oxide and other compounds. The arc is less stable than a cellulose electrode. It can be harder to maintain on the vertical position. The spatter is higher. However, the coating is designed to pull hydrogen out of the joint. It also provides a higher alloy content. This improves the mechanical properties of the weld.
Joint Design and Preheat Requirements
The joint design is a major factor in SMAW selection. A fillet weld on a thin gusset plate is different from a groove weld in a thick beam flange. The heat input and the cooling rate change the metallurgy of the weld.
Thick sections cool slowly. This is good. It reduces the risk of cracking. However, the heat input must be controlled. If you use too much heat, the heat affected zone can weaken. The base metal can lose its strength. For thick sections, you need a low-hydrogen electrode. You also need to preheat the joint. Preheat slows the cooling rate and reduces the risk of hydrogen cracking.
Thin sections cool quickly. This is dangerous. The weld metal can become hard. It can crack. For thin sections, you have more options. A cellulose electrode like 6013 might be acceptable if the steel is not too thick and the hydrogen risk is low. However, if the steel is high-strength, you still need a low-hydrogen electrode. You just use a smaller diameter to control the heat input.
Position and Accessibility
Welding position changes the difficulty. Horizontal and vertical welds require different arc lengths. Overhead welding is the hardest. The molten metal wants to fall. The arc wants to drift.
For overhead work, you need an electrode that is easy to strike and has a stable arc. Cellulose electrodes are often preferred here. They have a softer arc that is easier to control. Low-hydrogen electrodes can be difficult overhead. The arc can be stiff. The spatter can be higher. However, if the application requires low hydrogen, you must use it. You may need to adjust your technique. You might use a shorter arc length. You might use a smaller diameter.
The diameter of the electrode is also a factor. A 3/32 inch rod is easy to handle. A 7/32 inch rod is easier to control in overhead positions because the arc is larger. But it puts in more heat. For thick sections, you need the heat. For thin sections, you need to limit it.
Verifying Consumable Quality
A good electrode is useless if it is stored poorly. Electrodes are hygroscopic. They absorb moisture from the air. Moisture in the coating increases the hydrogen level. This defeats the purpose of a low-hydrogen electrode.
You must control the storage. Electrodes should be stored in a dry environment. In a shop, this means using a bake-out oven. You keep the electrodes at a low temperature, usually around 250 to 300 degrees Fahrenheit, to dry them out. You also limit the time they are out in the open. If they sit on the table for too long, they absorb moisture.
Check the packaging. The paper or plastic should be intact. If the package is torn or wet, the electrodes are suspect. Check the expiration date. Some coatings are not stable forever. If the electrodes are old, test them. Do a small coupon. Check the weld for porosity. If you see pinholes, the electrodes are wet.
Criteria for Selection
The table below summarizes the main criteria for selecting structural steel electrodes.
| Criterion | What to look for | Why it matters |
|---|---|---|
| Steel Grade | Match the electrode to the base metal tensile strength | Ensures the weld meets the structural load requirements |
| Hydrogen Content | Choose low-hydrogen for thick or high-strength steel | Prevents delayed cracking in load-bearing joints |
| Joint Thickness | Match electrode diameter to plate thickness | Controls heat input and prevents burn-through or lack of fusion |
| Welding Position | Choose coating based on arc stability needs | Ensures the welder can maintain a stable arc in all positions |
| Storage Condition | Verify dry storage and expiration dates | Prevents moisture absorption that causes porosity |
Decision Checklist
Before you start welding, run through this checklist.
- Identify the base metal grade and its required tensile strength.
- Determine the plate thickness and joint design.
- Check the welding position and accessibility.
- Select the electrode classification that matches the steel and conditions.
- Verify the electrode storage and dryness.
- Perform a weld on a test coupon.
- Inspect the weld for defects like porosity or cracks.
- Document the electrode lot number and the welder qualification.
Common Mistakes
Engineers often make a few common mistakes. The first is using the wrong diameter. Using a large rod on a thin plate causes burn-through. Using a small rod on a thick plate causes lack of fusion. The second mistake is ignoring preheat. If you weld thick steel without preheat, you invite cracking. The third is using wet electrodes. This is the most common cause of porosity. The fourth is not matching the electrode to the steel grade. A 6011 electrode is not a substitute for a 7018 on high-strength steel. The weld may look fine, but it may fail under load.
Final Thoughts
The choice of electrode is a technical decision. It is not a guess. By matching the chemistry to the steel and the conditions, you create a weld that performs. For structural steel, the stakes are high. A crack in a bridge or a building frame is not an option. Use the criteria above. Verify your consumables. And always test your process. The best electrode is the one that is selected correctly and used properly.
Frequently asked questions
Can I use 6013 instead of 7018 for structural steel?
Only for thin sections and low-strength steel. For thick or high-strength structural steel, 6013 has too much hydrogen and risks cracking.
How do I know if my electrodes are wet?
Look for porosity in the weld. If you see pinholes, the coating is wet. You can also test the arc. A wet electrode arcs poorly and spatters more.
What is the difference between 7016 and 7018?
Both are low-hydrogen. 7018 is the standard for high-strength steel. 7016 is similar but often has a slightly different coating recipe that may make it easier to strike.
Do I need to preheat for every structural weld?
No. Preheat depends on the thickness and the steel grade. Thin sections often do not need it. Thick sections and high-strength steels usually do.
How long can I keep an electrode out of the oven?
Keep it as short as possible. The longer it sits, the more moisture it absorbs. Most shops limit the time to a few minutes.